1. Overview of the Impact of Moisture on Tobacco
To understand the factors behind differences in the smoking quality of cigarettes with different moisture contents, changes in cut-tobacco moisture content, smoking quality, particulate- and gas-phase moisture in cigarette smoke, and volatile components of particulate matter were studied at equilibrium under different relative humidities. The results showed that:
① As the equilibrium ambient relative humidity rose from 30% to 70%, the moisture content of cut tobacco increased from 8.28% to 18.79%, and the smoking quality of the cigarettes changed from poor to good and back to poor. Cigarettes with moisture contents of 12.25% and 14.34% showed better smoking quality, while those at 8.28%, 9.13%, and 18.79% were poorer;
② As the moisture content of cut tobacco increased, both particulate-phase and gas-phase moisture in cigarette smoke showed an upward trend, with the gas-phase moisture rising more significantly;
③ Particulate matter and nicotine content decreased slightly as cut-tobacco moisture content increased, while CO increased significantly;
④ Cigarettes with moisture contents of 8.28%, 12.25%, and 18.79% all contained the same 70 volatile components in smoke particulate matter, but the 8.28% cigarettes had higher levels of readily volatile chemical components than the 12.25% cigarettes, while the 18.79% cigarettes had lower levels.
Therefore, cigarettes with a moisture content of 12%–14% deliver better smoking quality. Ambient humidity or cut-tobacco moisture content is an important factor affecting smoke moisture (especially gas-phase moisture) and low-molecular-weight volatile components, and ultimately sensory quality.
2. Application of Loss-on-Drying Moisture Analyzers in the Tobacco Industry
Loss-on-drying, also called the heated weight-loss method, is a physical method for determining moisture: heating drives off and dries out the water in the material. The traditional and most common approach is the oven method — the sample is dried in an oven, weighed on an electronic balance before and after, and the moisture value calculated by hand... Learn more about the loss-on-drying principle
Principle of Loss-on-Drying Moisture Analyzers
Loss-on-drying, also called the heated weight-loss method, is a physical method for determining moisture: heating drives off and dries out the water in the material. The traditional and most common approach is the oven method — the sample is dried in an oven, weighed on an electronic balance before and after, and the moisture value calculated by hand. One sample takes 2–4 hours to test this way; for fast-paced manufacturers the oven method seriously drags down production efficiency and no longer meets their needs.

Halogen heating technology heats up 40% faster than the conventional infrared heating technology on the market
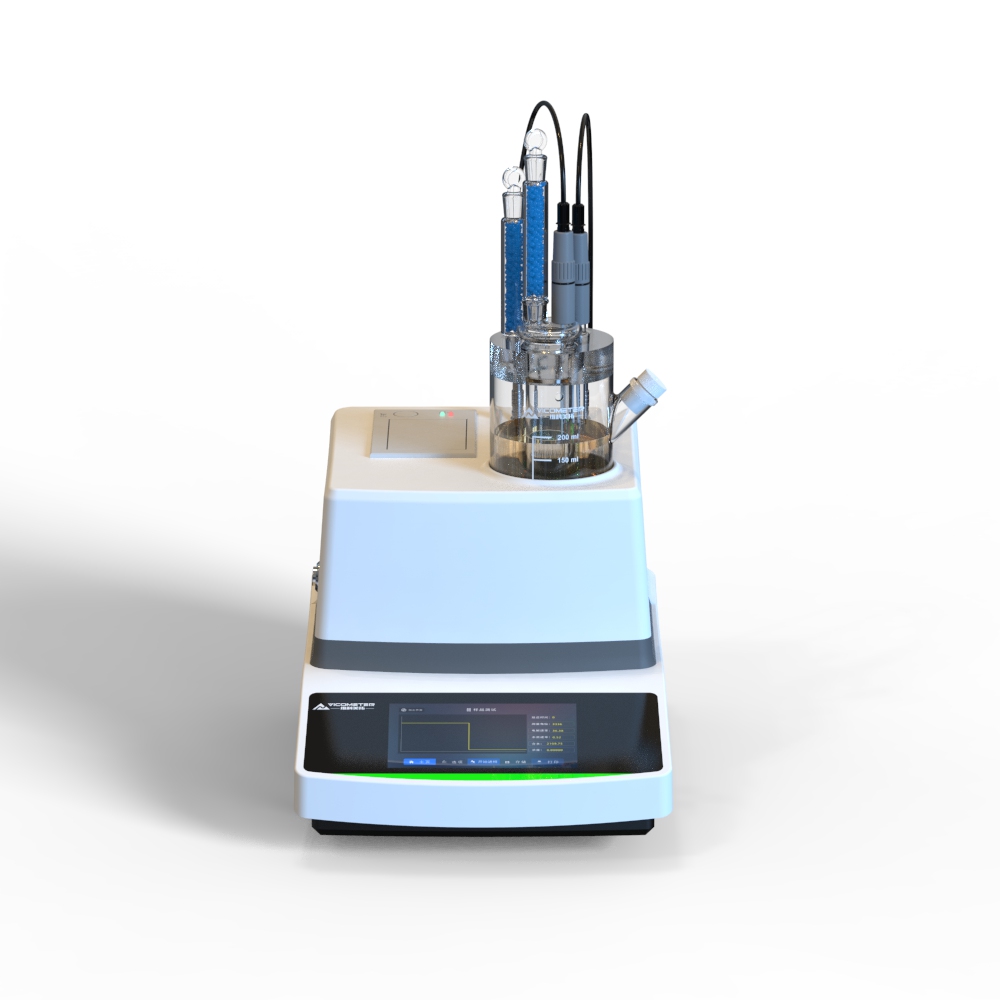
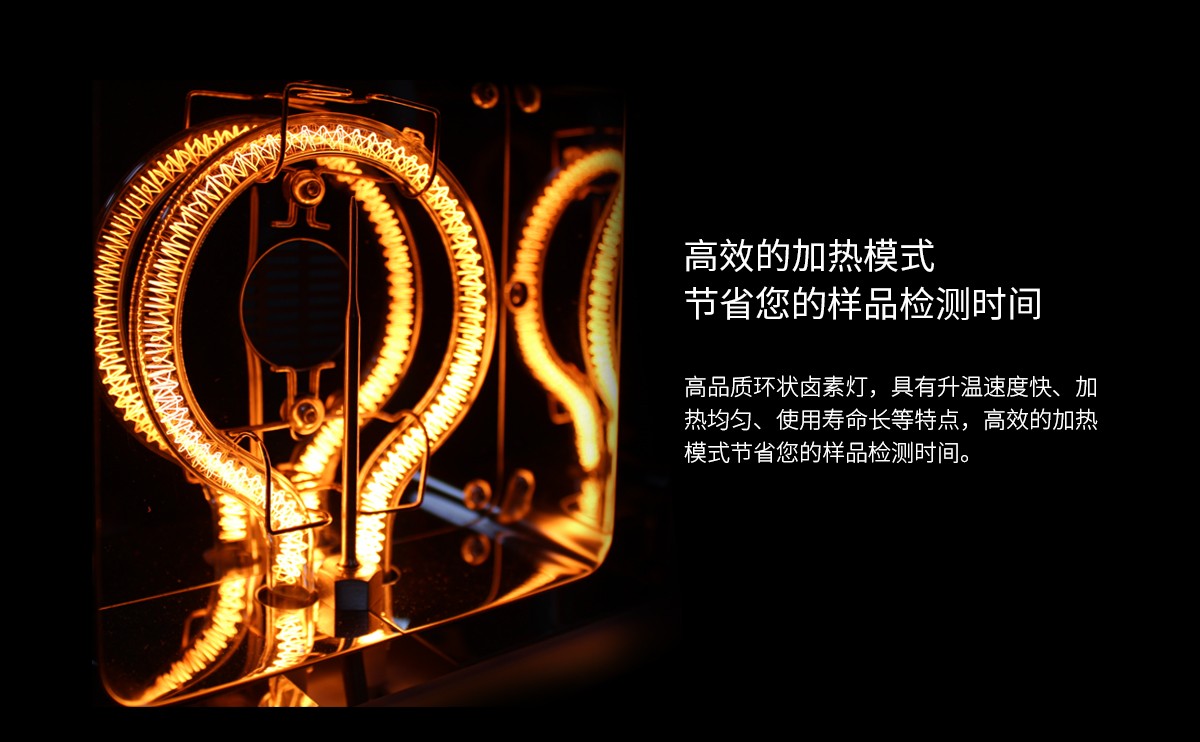
Against this backdrop, VicoMeter moisture analyzers use a highly efficient drying heater — a premium ring halogen lamp (far-infrared fast moisture analyzers use a far-infrared dark-field heater) — to heat samples in place of the traditional oven, heating quickly and evenly. The VicoMeter loss-on-drying fast moisture analyzer integrates and upgrades the oven-drying method, perfectly combining the heating, weighing, operation, and intelligent human-machine modules. The system stops intelligently based on the determination trend, analyzes the sample's moisture, and displays the result directly on screen — one-touch start delivers reliable results consistent with the oven method. A typical sample takes only minutes, far more efficient than the oven method, and these analyzers are widely favored and well reviewed by industrial users.
Based on different user needs, we offer the following solutions:
Halogen moisture analyzers and far-infrared dark-field heating moisture analyzers
Choose the instrument that suits your needs, or contact VicoMeter customer service directly for advice.
3. Application of Online Moisture Analyzers in the Tobacco Industry
An online moisture analyzer is an instrument that continuously monitors and displays product moisture in real time during production. In the tobacco industry, microwave and infrared are the two main solutions. An online moisture analyzer is also a rapid moisture detection option; unlike a portable moisture analyzer, it can be installed directly at the worksite for real-time moisture monitoring. Enterprises can analyze historical data to refine production processes and use the moisture alarm function for rapid handling of on-site over-limit moisture, supporting stable production and playing a vital role in manufacturing operations...Learn More About the Principle of Online Moisture Analyzers
Principle of Online Near-Infrared Moisture Analyzers
O-H bonds in water and C-H bonds in organics absorb NIR light at specific wavelengths; reflected energy is inversely proportional to absorbing molecules. The analyzer tracks NIR energy changes at a specific wavelength based on water's absorption.
Water molecules vibrate at specific energy bands—O-H bonds stretching, contracting, twisting. NIR bands are especially strong for water and easy to generate, filter, and detect; moisture-measuring wavelengths stay within 1-2.5 μm.
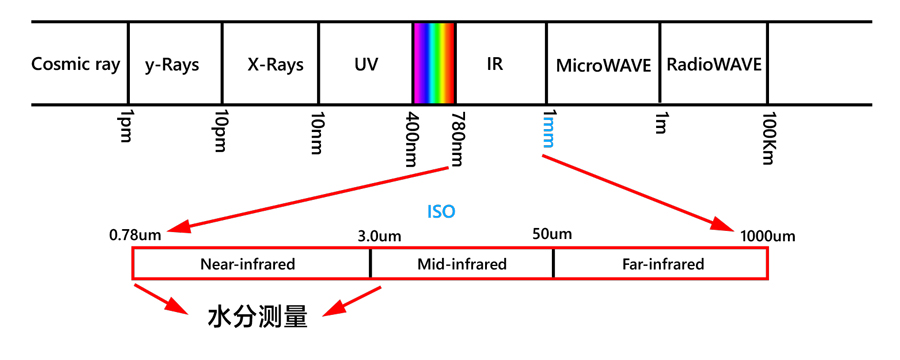
Absorption depends on water molecules encountered and absorption strength—proportional to moisture. As a reflectance method it is also affected by the material's reflectance and absorption; NIR measurement is non-destructive, non-contact, and real-time.
Working Principle of Online Near-Infrared Moisture Monitoring Systems
Multiple NIR beams focus onto the material surface; reflected beams are received by an advanced optical detection system with an embedded high-performance DSP chip for fast processing, storage, and display—outstanding accuracy and stability.
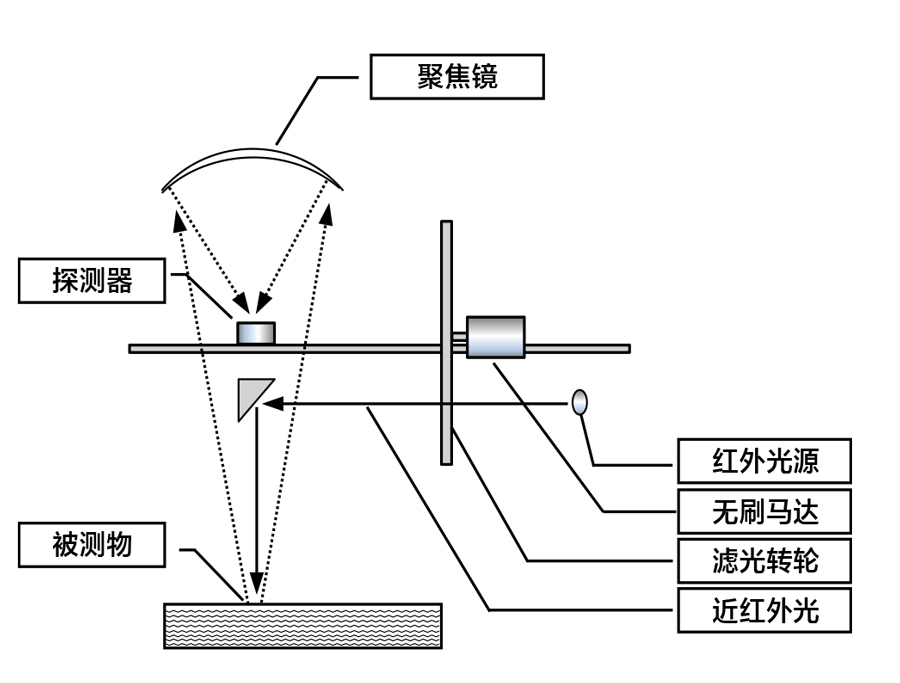
Many materials absorb infrared at specific wavelengths only; at least two are selected—a reference wavelength (not absorbed by material or water) and a measurement wavelength (absorbed by water only).
Precision filters on a rotating wheel pass reference and measurement pulses alternately onto the sample; the two timed pulses reflect to a detector as two signals. The reference shows expected reflection; the measurement is attenuated by water absorption. Combined into a ratio, differences from other moisture levels are proportional to moisture differences.
The signal strengths of the two channels combine into: R/M X M1/R1=ratio
Where: R--reference channel of the product beam
M--measurement channel of the product beam
M1--measurement channel of the compensation beam
R1--reference channel of the compensation beam
If drift occurs, M and M1 shift equally, canceling out in the ratio and preserving stability.
Principle of Online Microwave Moisture Analyzers
Microwave attenuation and phase shift depend on the medium's dielectric constant and loss tangent—far higher for polar water than ordinary media. Moisture is calculated from received attenuation and phase shift.
Because microwaves completely penetrate the process material, all physically bound moisture can be measured — both surface moisture and internal moisture. This technology ensures high measurement accuracy and precision, and the color and surface structure of the material do not affect the results. It is widely applicable to coal, sintered (pellet) blends, iron ore, chemicals, bauxite, nickel ore, sugar, tobacco, bagasse, grain, silicon, wood, wool, sand, polymers, cotton, and other non-conductive materials.
A Detailed Look at Online Microwave Moisture Analyzers
The probe measures 150-200 mm deep, analyzing total (core and surface) moisture; deep penetration means surface dirt does not matter.
The variation of relative permittivity is the key principle; simply:
Water's εr≈80 versus ~1-10 for most materials (sand/gravel 3-4)—a large measurable difference.
Moisture is measured directly from this difference and output as a mass-percentage standard signal.
In other words: the more water a material contains, the closer its relative permittivity εr approaches 80.
Signals are obtained as material passes the sensor—even on fast lines; stationary bulk materials can also be measured.
Based on different user needs, we offer the following solutions:
NIR Online Moisture Meter
Online Microwave Moisture Analyzer
Choose the instrument that suits your needs, or contact VicoMeter customer service directly for advice.
4. Application of Portable Moisture Analyzers in the Tobacco Industry
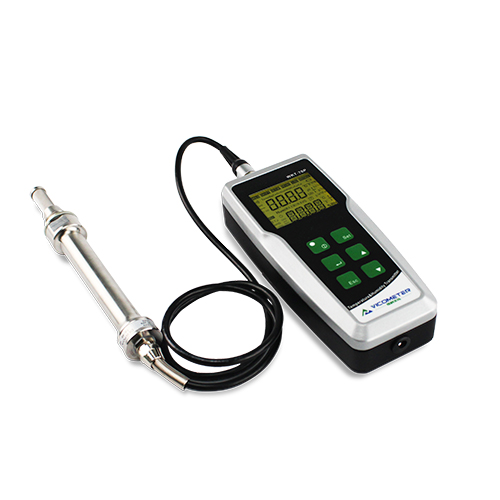
A portable moisture analyzer is an instrument for rapid moisture detection of materials. Its overall accuracy is lower than that of laboratory moisture analyzers, but it is more reliable and accurate than the feel and experience of a veteran worker. A calibrated portable moisture analyzer can quickly determine a sample's moisture content on site; if the moisture content of tobacco material exceeds the alarm threshold, the sample is sent to a professional laboratory for confirmation with a laboratory moisture analyzer. Thanks to their portability and fast testing, portable moisture analyzers are widely used in incoming material inspection, production sites, and spot checks in the tobacco industry.
5. Application of Dew Point Moisture Analyzers in the Tobacco Industry
Using the resistive-capacitive method, the sensor rapidly displays dew point/humidity in full gas contact. It mounts on lines or travels to the field—no consumables—covering storage/transport ambient gases and process gases/equipment to catch problems early.